📐"前 50 个企业查询可获得定制 3D 仓库设计" 计划


Why Heavy-Duty Racking is Essential for Manufacturing
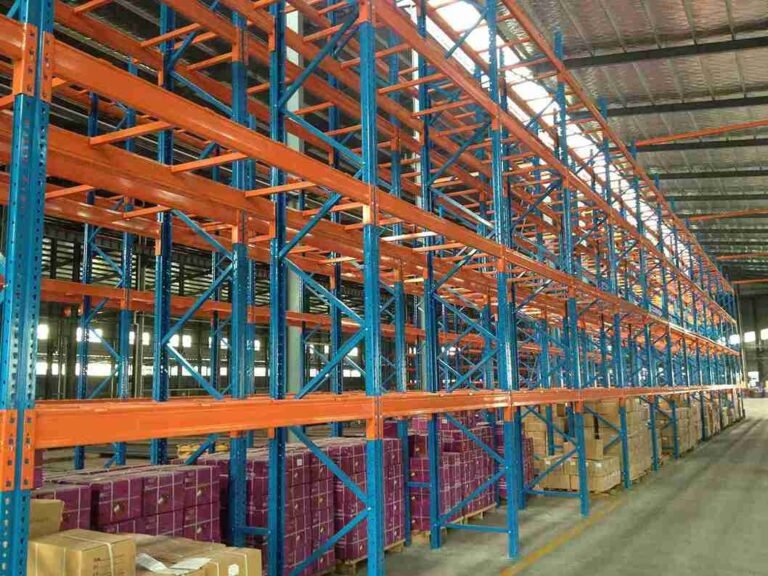
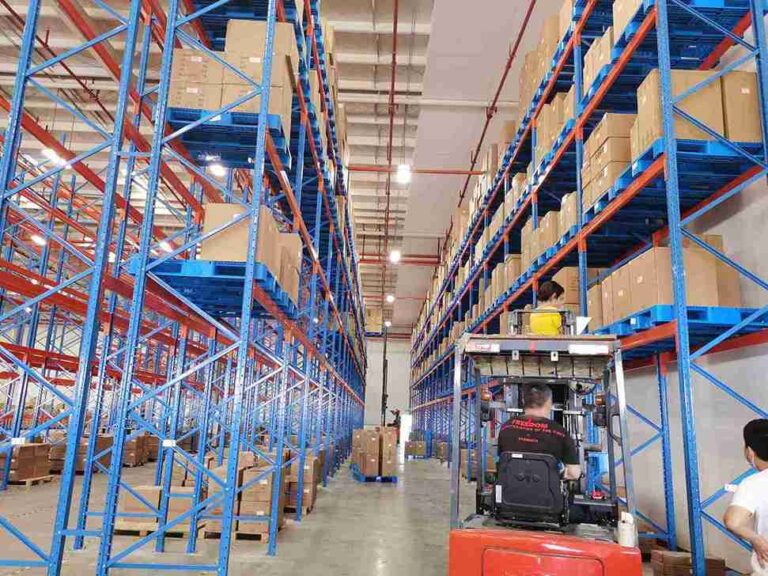
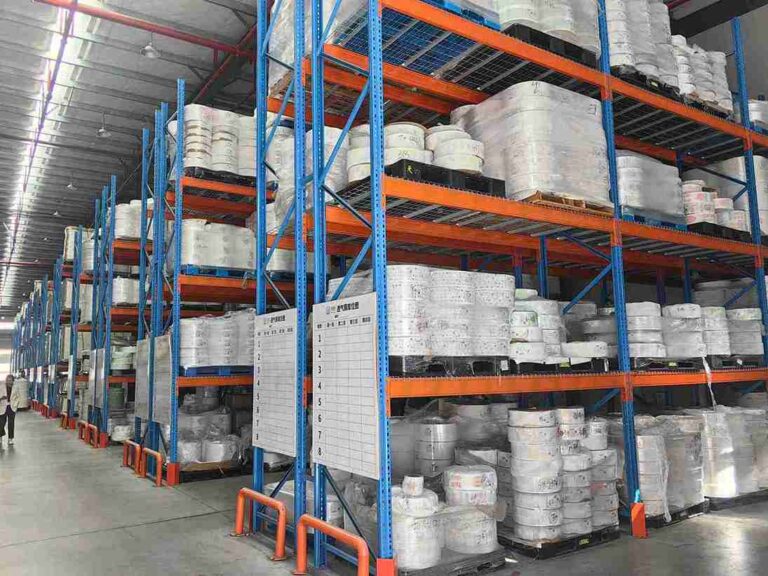
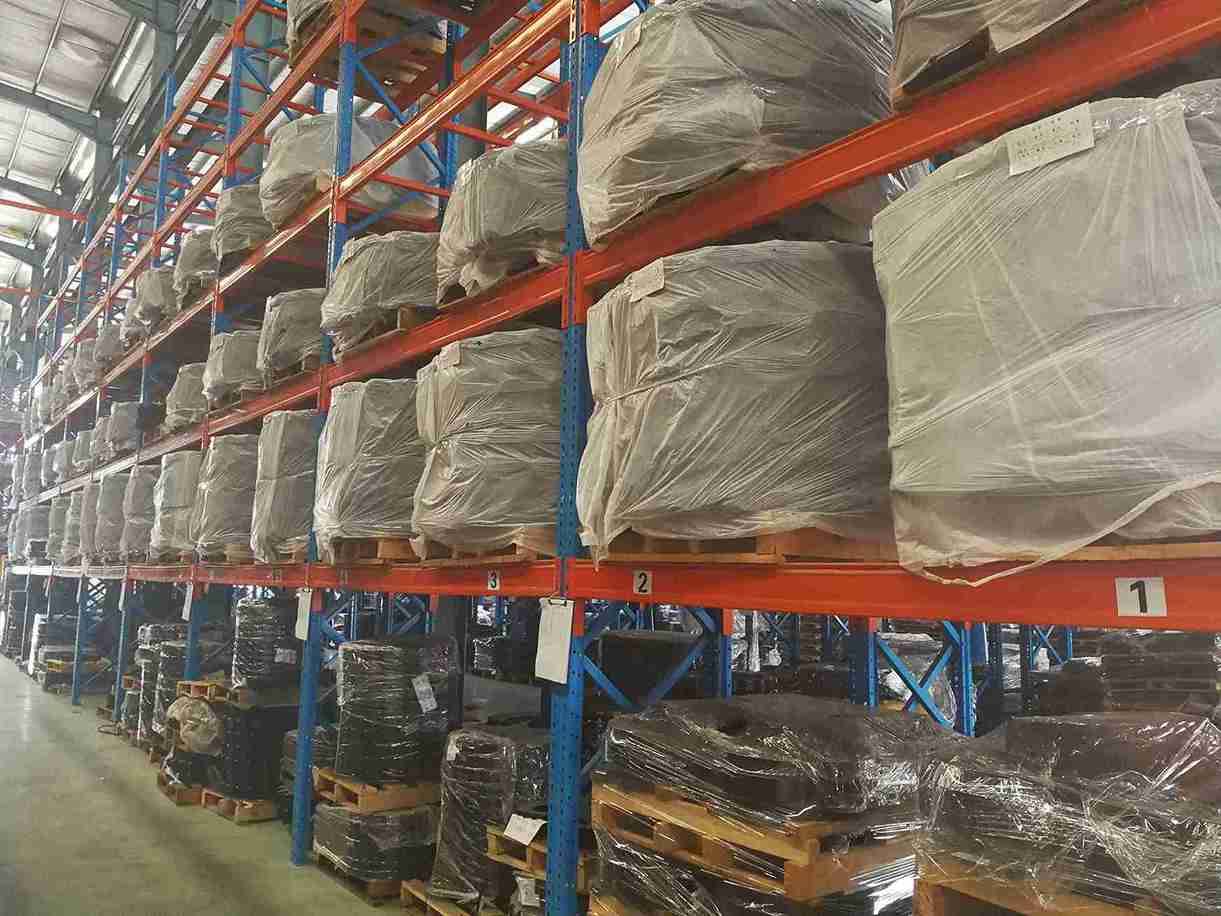
Every high-performance manufacturing facility relies on heavy-duty racking for manufacturing operations to maximize storage efficiency, improve workflow, and ensure workplace safety. Unlike standard shelving, heavy-duty racking for manufacturing plants is engineered to withstand extreme loads, frequent forklift traffic, and harsh industrial conditions.
This guide dives deep into the world of heavy-duty racking for manufacturing, covering:
- The best racking systems for different manufacturing needs
- Key benefits of industrial-grade storage solutions
- How to select, install, and maintain heavy-duty racking
- Top manufacturers and future industry trends
Whether managing raw materials, work-in-progress inventory, or finished goods, the right heavy-duty racking for manufacturing can transform warehouse operations.
1. What Makes Heavy-Duty Racking Different for Manufacturing?
Heavy-duty racking for manufacturing isn’t just about strength—it’s about precision engineering for industrial demands.
1.1. Core Features of Manufacturing-Grade Racking
- Ultra-high load capacity (5,000–50,000 lbs per shelf)
- Reinforced steel construction (12–16 gauge steel with protective coatings)
- Forklift-accessible designs for seamless material handling
- Adjustable configurations to adapt to changing production needs
1.2. How Heavy-Duty Racking Outperforms Standard Shelving
| 特点 | Standard Shelving | Heavy-Duty Racking for Manufacturing |
|---|---|---|
| Load Capacity | 500–2,000 lbs | 5,000–50,000+ lbs |
| Durability | Light-duty steel | Industrial-grade reinforced steel |
| Forklift Compatibility | 没有 | Yes (most systems) |
| Seismic/Wind Rating | Rarely | Often compliant |
2. Top 5 Heavy-Duty Racking Systems for Manufacturing
Not all heavy-duty racking for manufacturing is the same. The best system depends on storage density, accessibility, and workflow needs.
2.1. Selective Pallet Racking – The Manufacturing Workhorse
- 最适合 Facilities needing direct access to every pallet
- Max Weight: 3,000–6,000 lbs per shelf
- Key Benefit: Flexible layout options (narrow aisle, wide aisle, double-deep)
Example Use Case:
A automotive parts manufacturer uses selective pallet racking to store engine components, allowing forklifts to retrieve specific SKUs quickly.
2.2. Drive-In/Drive-Through Racking – High-Density Storage
- 最适合 Bulk storage of uniform products (e.g., beverages, packaged goods)
- Max Weight: 4,000–10,000 lbs per level
- Key Benefit: 60% more storage density than selective racking
专业提示
Drive-in racking follows LIFO (Last-In, First-Out), while drive-through allows FIFO (First-In, First-Out) access.
2.3. Cantilever Racking – For Oversized Manufacturing Materials
- 最适合 Long, bulky items (steel bars, pipes, lumber)
- Max Weight: 20,000–50,000 lbs per arm
- Key Benefit: No front columns for easy loading/unloading
Industry Example:
A metal fabrication plant uses cantilever racking to store 20-foot steel beams without obstruction.
2.4. Push-Back Racking – High-Density with Selectivity
- 最适合 Multi-SKU storage needing moderate selectivity
- Max Weight: 2,500–5,000 lbs per lane
- Key Benefit: Dynamic storage with less aisle space than drive-in systems
2.5. Pallet Flow Racking – Automated FIFO Storage
- 最适合 Perishable goods or high-rotation inventory
- Max Weight: 1,500–4,000 lbs per lane
- Key Benefit: Gravity-fed movement reduces forklift travel time
3. The Unmatched Benefits of Heavy-Duty Racking for Manufacturing
Why do leading manufacturing plants invest in heavy-duty racking systems?
3.1. Space Optimization = Cost Savings
- Vertical storage utilizes 40% more cubic space than floor stacking
- Narrow aisle configurations reduce wasted aisle space
3.2. Enhanced Workplace Safety
- Industrial-grade steel prevents collapses under heavy loads
- Seismic bracing protects against earthquakes (critical for facilities in California, Japan, etc.)
3.3. Faster Material Handling = Higher Productivity
- Forklift-optimized layouts cut retrieval time by 30–50%
- Automated systems (like pallet flow) reduce manual labor
3.4. Long-Term ROI
- 20–30 year lifespan with proper maintenance
- 模块化设计 allow easy expansion
4. How to Choose the Best Heavy-Duty Racking for Your Facility
Selecting heavy-duty racking for manufacturing requires careful planning.
4.1. Step 1: Assess Your Storage Needs
- What’s your average pallet weight? (Light: <1,500 lbs, Heavy: 5,000+ lbs)
- How often is inventory rotated? (Daily FIFO vs. monthly LIFO)
4.2. Step 2: Evaluate Your Warehouse Layout
- Ceiling height (Taller facilities can use multi-tier racking)
- Forklift turning radius (Determines aisle width)
4.3. Step 3: Compliance & Safety Checks
- OSHA & ANSI standards for load signage and column protection
- Seismic zone requirements (if applicable)
5. Installation & Maintenance: Keeping Your Racking in Peak Condition
Even the best heavy-duty racking for manufacturing needs proper care.
5.1. Professional Installation vs. DIY
- Pros hire structural engineers to ensure perfect alignment
- DIY risks: Uneven weight distribution, safety hazards
5.2. Essential Maintenance Checklist
✅Monthly inspections for bent beams or loose bolts
✅Annual re-torquing of all connections
✅Immediate repairs on any damaged components
5.3. Safety Upgrades Worth Considering
- Column guards to prevent forklift collisions
- Anti-slip decking for worker safety
6. The Future of Heavy-Duty Racking for Manufacturing
Emerging trends shaping the industry:
- AI-powered inventory tracking (smart sensors on racks)
- Automated storage & retrieval systems (AS/RS)
- Sustainable steel with recycled materials
Conclusion: Is Heavy-Duty Racking Right for Your Facility?
For manufacturing plants handling heavy loads, heavy-duty racking isn’t optional—it’s a strategic investment. The right system improves space utilization, safety, and efficiency, directly impacting the bottom line.
Next Steps:
- Consult a racking specialist for a custom quote
- Schedule a warehouse audit to determine optimal layout
- Compare top manufacturers (Steel King, Ridg-U-Rak, UNARCO)
常见问题: Heavy-Duty Racking for Manufacturing
1. How much does heavy-duty racking for manufacturing cost?
Prices range from 1,000 per pallet position, depending on capacity and features.
2. Can existing warehouses be retrofitted with heavy-duty racking?
Yes, but a structural engineer should assess floor strength first.
3. What’s the lifespan of heavy-duty racking?
With maintenance, 20–30 years—longer than most manufacturing equipment.
4. How do I know if my racking is overloaded?
Warning signs: beam deflection, leaning frames, or audible creaking.
5. Are there fireproof heavy-duty racking options?
Some manufacturers offer fire-resistant coatings, but sprinklers are more effective.
This guide ensures you make the best choice in heavy-duty racking for manufacturing—boosting efficiency while keeping workers safe. 🚀