📐 "Eerste 50 bedrijfsvragen krijgen aangepast 3D-ontwerp van magazijn" Plan



Inleiding
In today’s fast-paced industrial and commercial environments, ruimteoptimalisatie is a critical challenge. Mobile shelving racks have emerged as one of the most efficient storage solutions, allowing businesses to maximize floor space while maintaining easy access to stored items. Unlike traditional static shelving, mobile shelving systems operate on a track-based mechanism, enabling entire shelving units to move laterally, eliminating unnecessary aisles and significantly increasing storage density.
This comprehensive guide explores the benefits, types, applications, and best practices for implementing mobile shelving racks in warehouses, archives, retail spaces, and more. Whether you’re looking to reduce operational costs, improve inventory management, or optimize warehouse space, this article provides bruikbare inzichten backed by industry expertise.
1. What Are Mobile Shelving Racks?
1.1 Definition and Core Mechanism
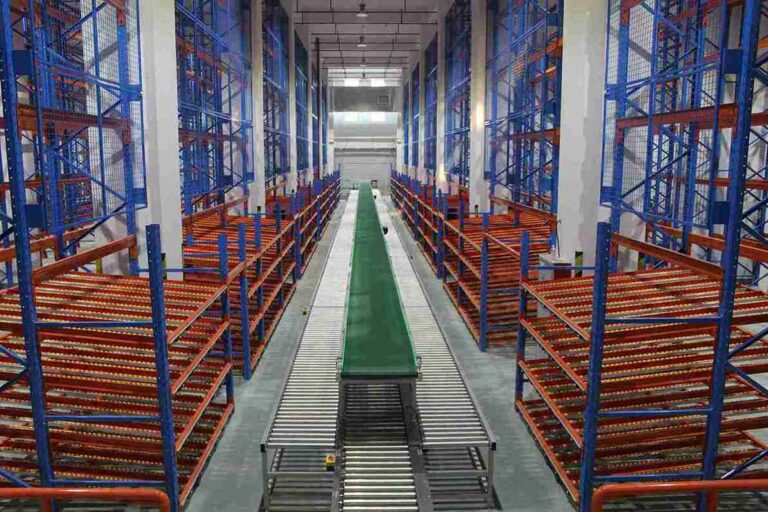
Mobile shelving racks (also known as compact shelvingofmovable shelving systems) are opslagoplossingen met hoge dichtheid designed to minimize wasted space. Unlike fixed shelving, these systems operate on motorized or manual tracks, allowing shelves to be compacted together when not in use.
- Track-Based Movement: Shelves glide smoothly on heavy-duty rails, reducing the need for multiple aisles.
- Manual vs. Motorized Systems: Some models require manual pushing, while others use electric-powered movement for effortless operation.
- Space Efficiency: By eliminating fixed aisles, businesses can increase storage capacity by up to 100%.
1.2 Key Components of Mobile Shelving Systems
A well-designed mobile shelving system consists of:
- Base Frame & Carriages: Provides structural stability and smooth movement.
- Rollers & Tracks: Ensures seamless sliding with minimal friction.
- Safety Brakes & Sensors: Prevents accidental movement and enhances workplace safety.
- Shelving Bays: Adjustable configurations to accommodate different load types.
2. Benefits of Mobile Shelving Racks
2.1 Maximized Storage Capacity
The primary advantage of mobile shelving racks is their ability to dramatically increase storage density. Traditional shelving requires fixed aisles, whereas compact shelving eliminates unnecessary walkways, allowing for more storage in the same footprint.
2.2 Improved Accessibility & Organization
Despite their high-density design, mobile shelving systems provide easy access to stored items. Features like:
- Push-button operation (for motorized systems)
- Locking mechanisms to secure shelves in place
- Customizable shelving heights for different inventory types
2.3 Enhanced Workplace Safety
Modern mobile shelving racks incorporate:
- Anti-tip mechanisms
- Emergency stop buttons
- Weight sensorsom overbelasting te voorkomen
2.4 Cost-Effective Space Utilization
By reducing the need for additional warehouse space, businesses can lower real estate costsmet behoud vanefficient inventory management.
3. Types of Mobile Shelving Racks
3.1 Manual Mobile Shelving
- Best for: Small to medium-sized businesses with moderate storage needs.
- Operation: Requires physical pushing to move shelves.
- Cost: More affordable than motorized options.
3.2 Motorized Mobile Shelving
- Best for: Large warehouses, archives, and high-traffic facilities.
- Operation: Powered by electric motors for effortless movement.
- Features: Remote control, automated positioning, and integration with warehouse management systems (WMS).
3.3 High-Density Mobile Racking
- Ideal for: Heavy-duty industrial storage.
- Capacity: Supports palletized loads and bulk storage.
3.4 Mobile Shelving for Archives & Document Storage
- Specialized for: Libraries, medical records, legal documents.
- Features: Dust-resistant, fireproof options available.
4. Applications of Mobile Shelving Racks
4.1 Warehousing & Logistics
- Pallet racking alternatives for high-density storage.
- Cold storage optimization for perishable goods.
4.2 Retail & Backroom Storage
- Space-saving solutions for stockrooms.
- Adjustable shelving for seasonal inventory changes.
4.3 Healthcare & Pharmaceutical Storage
- Secure storage for medical supplies.
- Compliance with safety regulations.
4.4 Industrial & Manufacturing
- Tool and equipment storage.
- Heavy-duty shelving for machinery parts.
5. How to Choose the Right Mobile Shelving System
5.1 Assess Your Storage Needs
- Inventory type (documents, pallets, small parts).
- Frequency of access (daily retrieval vs. long-term storage).
5.2 Consider Floor Load Capacity
- Ensure flooring can support the system’s weight.
- Reinforced concrete floors are ideal for heavy-duty systems.
5.3 Evaluate Safety Features
- Look for UL-certified systems in fire-prone environments.
- Anti-collision sensors for busy warehouses.
5.4 Budget & ROI Considerations
- Manual vs. motorized cost comparison.
- Long-term savings from reduced space requirements.
6. Installation & Maintenance Best Practices
6.1 Professional Installation
- Hire certified installers to ensure proper alignment.
- Floor preparation (leveling, reinforcement).
6.2 Routine Maintenance Tips
- Lubricate tracks for smooth operation.
- Inspect rollers and brakes periodically.
7. Future Trends in Mobile Shelving Technology
7.1 Smart Shelving & IoT Integration
- Automated inventory tracking.
- AI-powered space optimization.
7.2 Sustainable Materials & Designs
- Eco-friendly manufacturing.
- Energy-efficient motorized systems.
Conclusie
Mobile shelving racks represent a revolutionary approach to space-saving storage, offering unparalleled efficiency for warehouses, archives, retail spaces, and industrial facilities. By eliminating wasted aisle space, these systems maximize storage capacity while improving accessibility and safety.
Whether you opt for manual or motorized mobile shelving, selecting the right system depends on your specific storage needs, budget, and operational workflow. With advancements in smart shelving and IoT integration, the future of compact storage solutions is set to become even more efficient.
For businesses looking to optimize storage space, reduce costs, and enhance inventory management,mobile shelving racks are the ultimate solution.
FAQs
1. How much weight can mobile shelving racks support?
Depending on the model, mobile shelving systems can support up to 1,000 lbs per shelf, with heavy-duty industrial versions handling even more.
2. Are mobile shelving systems difficult to maintain?
No, routine maintenance is simple—lubricating tracks and inspecting rollers ensures smooth operation.
3. Can mobile shelving be installed in existing warehouses?
Yes, but floor reinforcement may be required for heavy-duty systems.
4. What industries benefit most from mobile shelving?
Warehousing, healthcare, retail, and archives see the greatest efficiency gains.
5. Are there fireproof mobile shelving options?
Yes, UL-listed fire-resistant models are available for document storage.